Point Angle
Standard 118° point angles suit soft metals and general steel. Steeper 135° to 140° point angles shorten chip length and reduce work-hardening in stainless steel and titanium.
This technical guide details the core principles of drill bit design, web thinning techniques, flute geometries, and custom tool engineering for high-performance holemaking.
Optimizing the design of CNC drill bits is essential for achieving straight hole axes, excellent surface finishes, and maximum tool life. Holemaking presents unique chip-evacuation and thermal-friction challenges because cutting velocity drops to zero at the absolute center of the tool. Effective CNC drilling tools balance web strength, point self-centering capability, and open flute volume for continuous chip evacuation.
Standard 118° point angles suit soft metals and general steel. Steeper 135° to 140° point angles shorten chip length and reduce work-hardening in stainless steel and titanium.
S-gash or split-point web thinning reduces axial thrust forces, limits tool wander, and allows a CNC drill setup to self-center without spot drilling.
A heavy central web increases beam strength to resist deflection during deep-hole drilling, while a back taper reduces friction along the margin.
Double-margin designs provide secondary support along the hole wall, improving hole straightness and roundness in deep-hole applications.
Efficient chip evacuation helps prevent chip packing, tool breakage, and hole-wall scarring during continuous drilling cycles.
Open, curved flute profiles increase chip space and allow deep-hole drilling up to 10×D to 30×D without frequent pecking cycles.
Helical internal coolant holes deliver high-pressure fluid directly to the cutting lips, rapidly flushing chips while cooling the chisel edge.
Mirror-finished flute surfaces reduce friction and help prevent chip welding in sticky non-ferrous aluminum and copper alloys.
Use high helix angles of 30°–38°, ultra-sharp cutting edges, polished open flutes, and DLC or ZrN coatings to eliminate material galling.
Heavy web cores, 140° split points, micro-honed cutting edges, and AlTiN or nACo coatings withstand heat and work-hardening.
Flat 140° point angles, reinforced corner chamfers, and high-wear carbide substrates resist abrasive margin wear.
Specialized double-angle or dagger-point geometries shear abrasive fibers cleanly to prevent exit delamination and burring.
Bauron manufactures a complete range of drilling tools, grouped by application. Each category diagram below is paired with the specific drill types it contains.
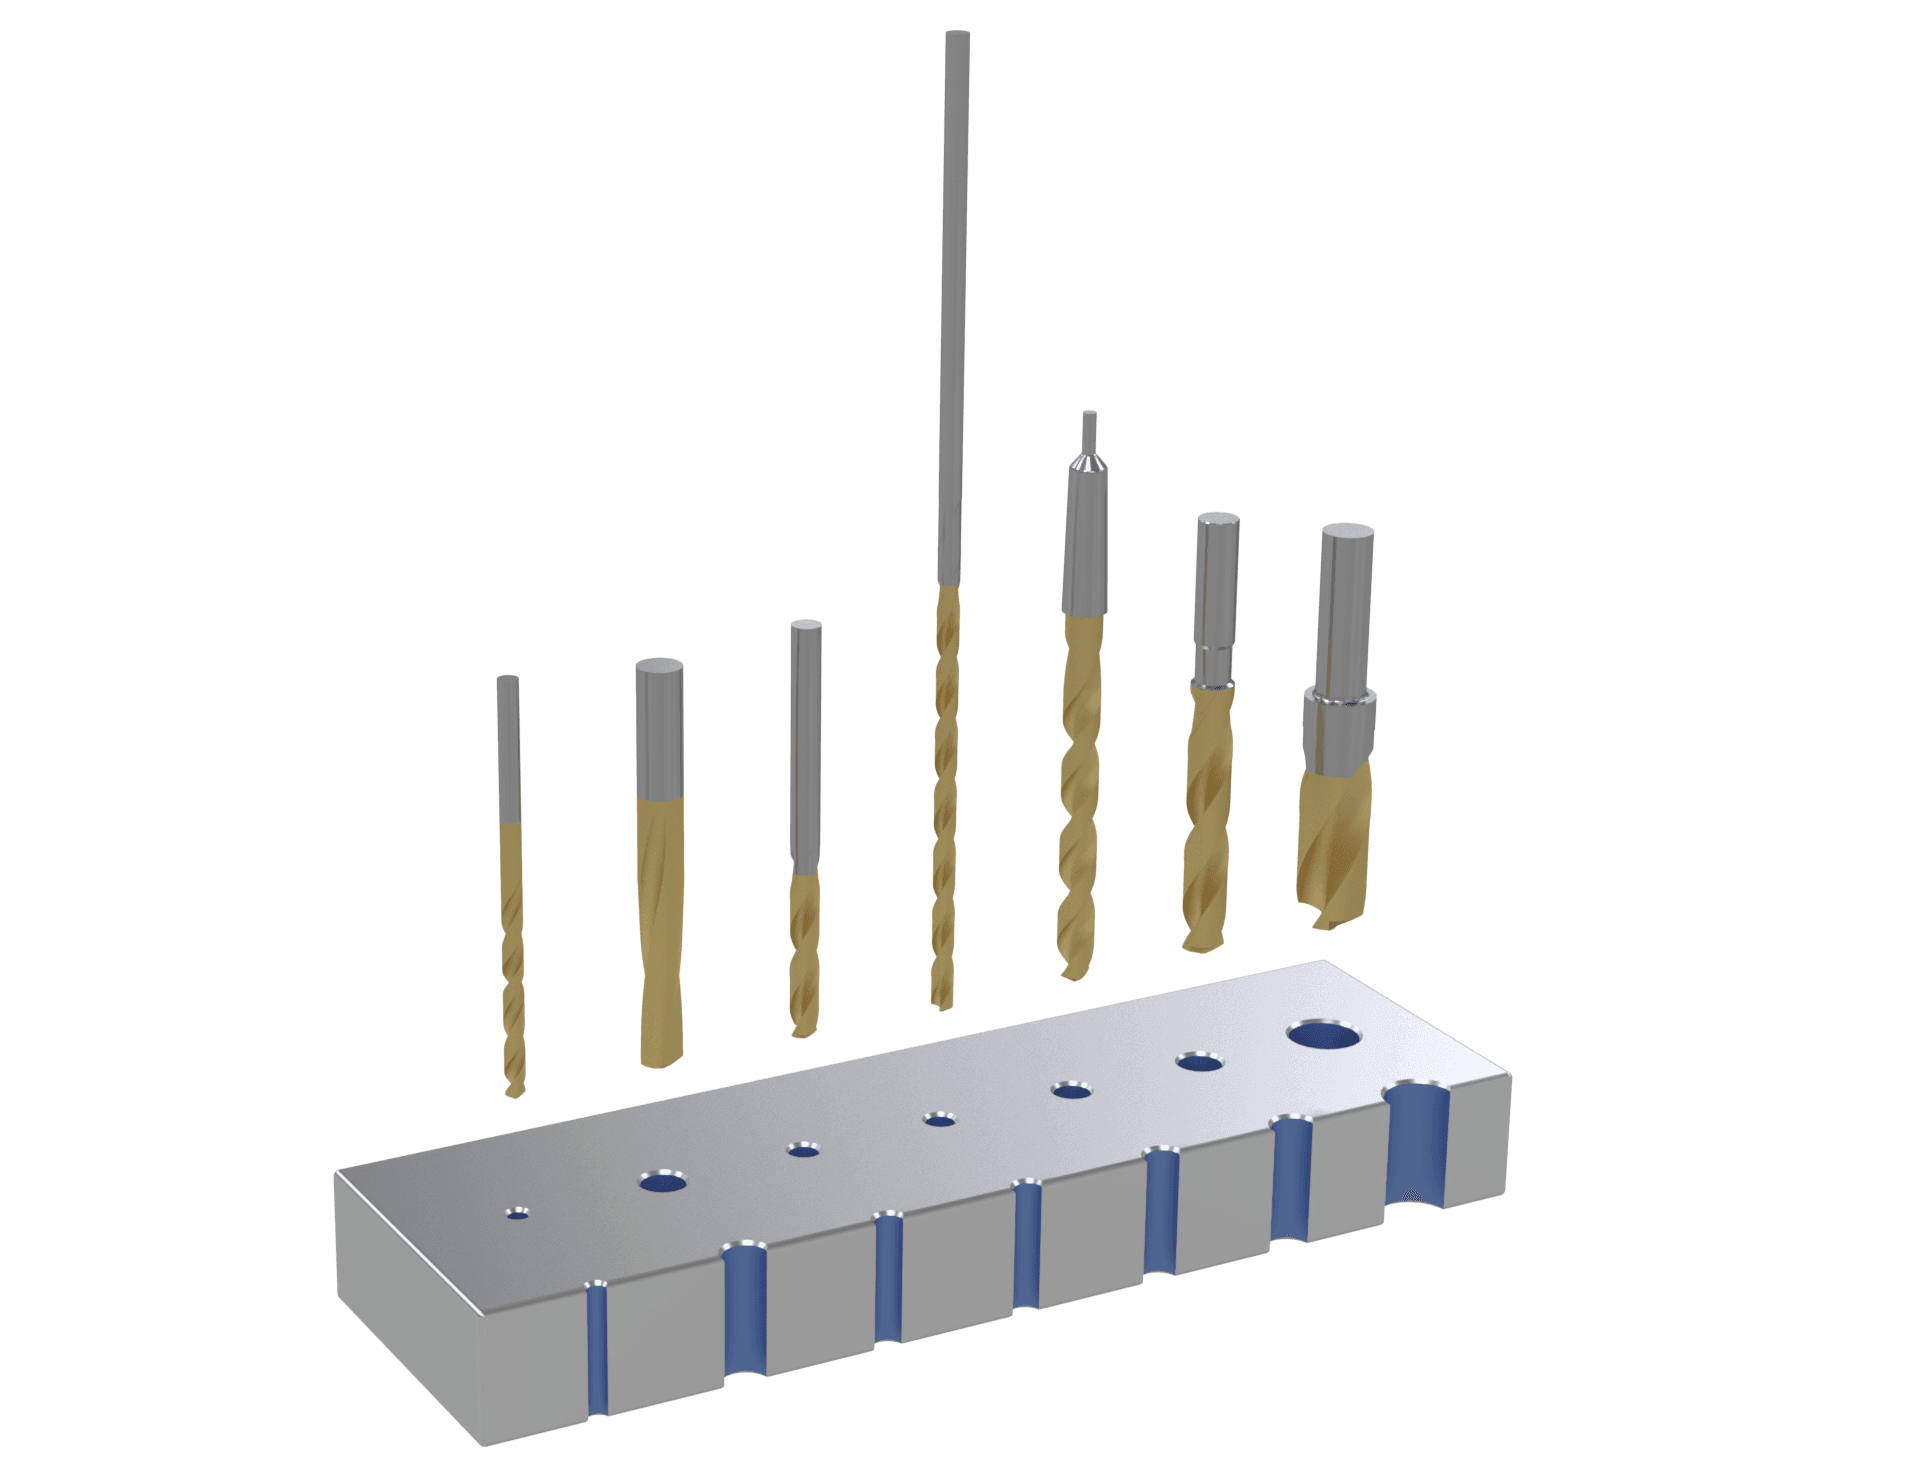
Versatile drills for everyday holemaking across a wide range of materials.
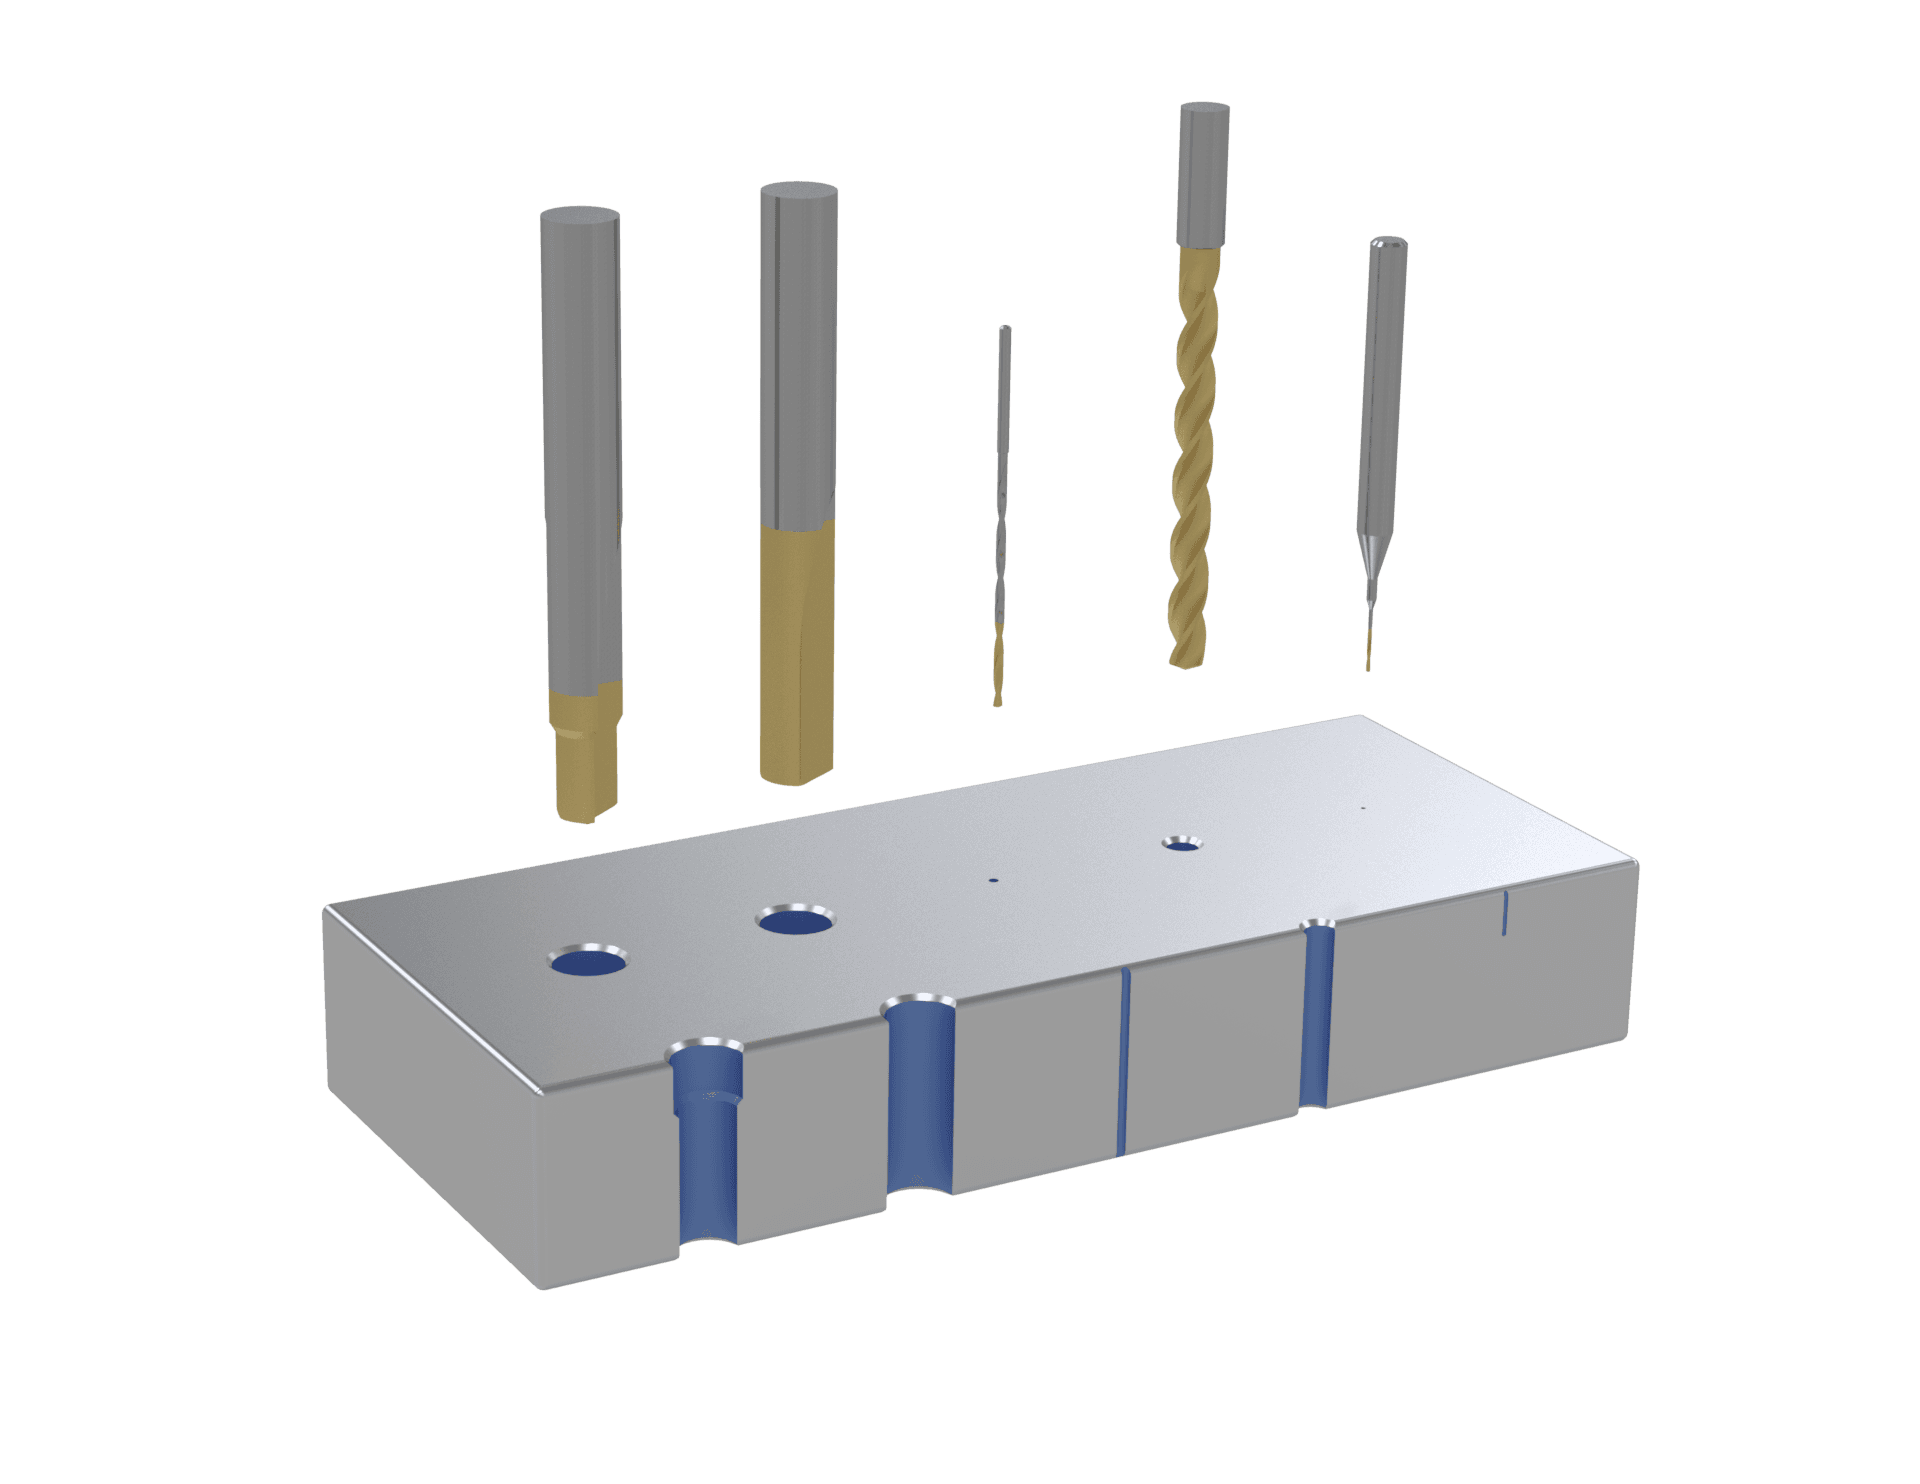
Specialized flute geometries and micro sizes for demanding or delicate work.
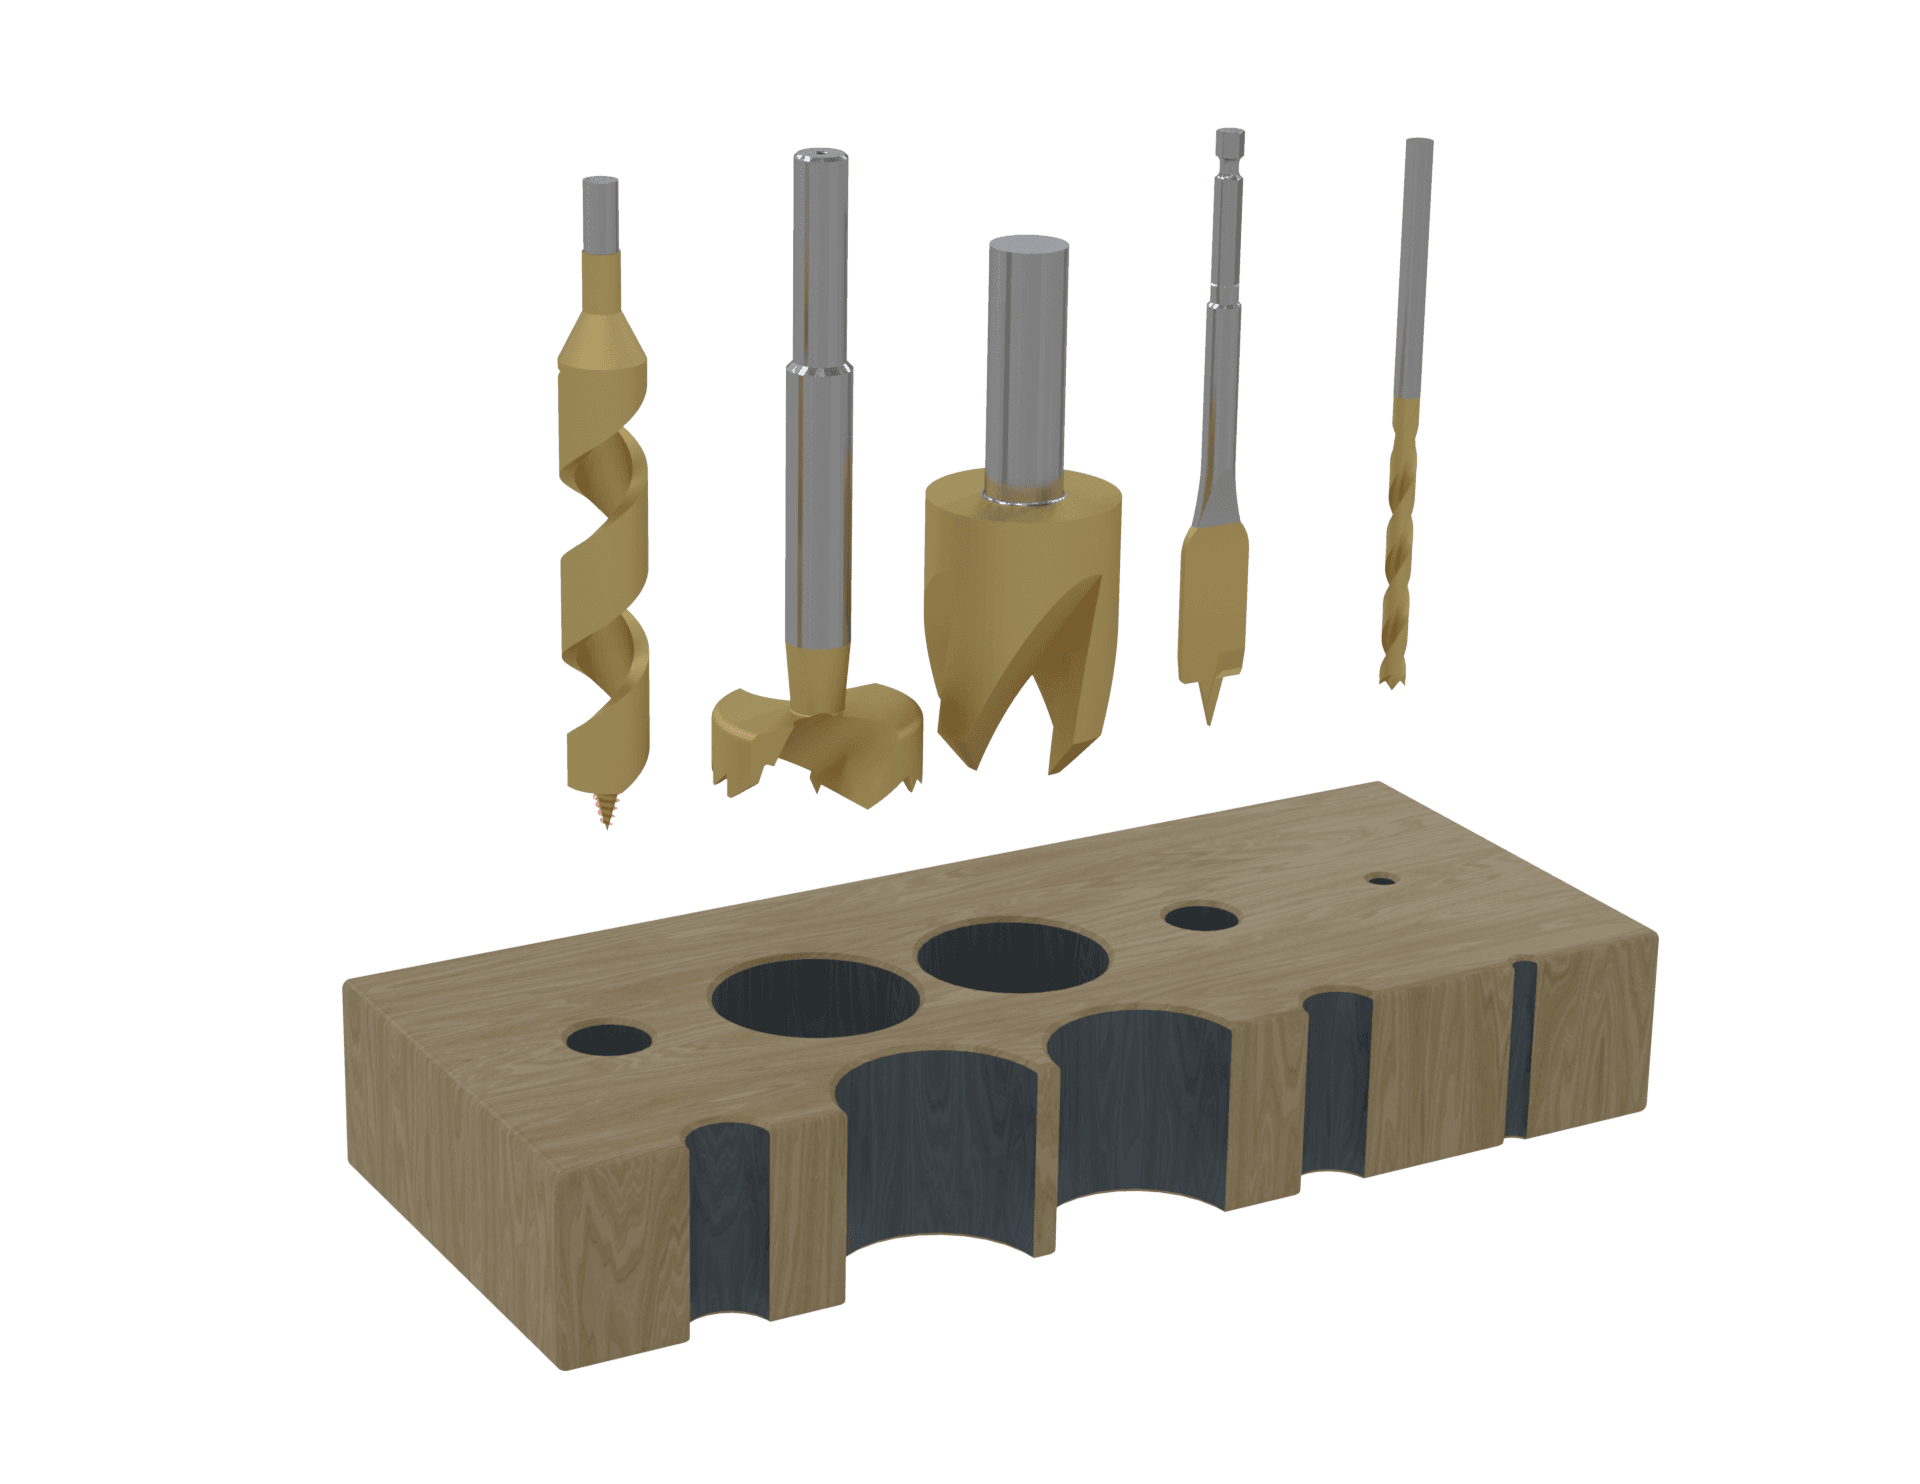
Purpose-built geometries for clean, controlled holes in wood and soft materials.
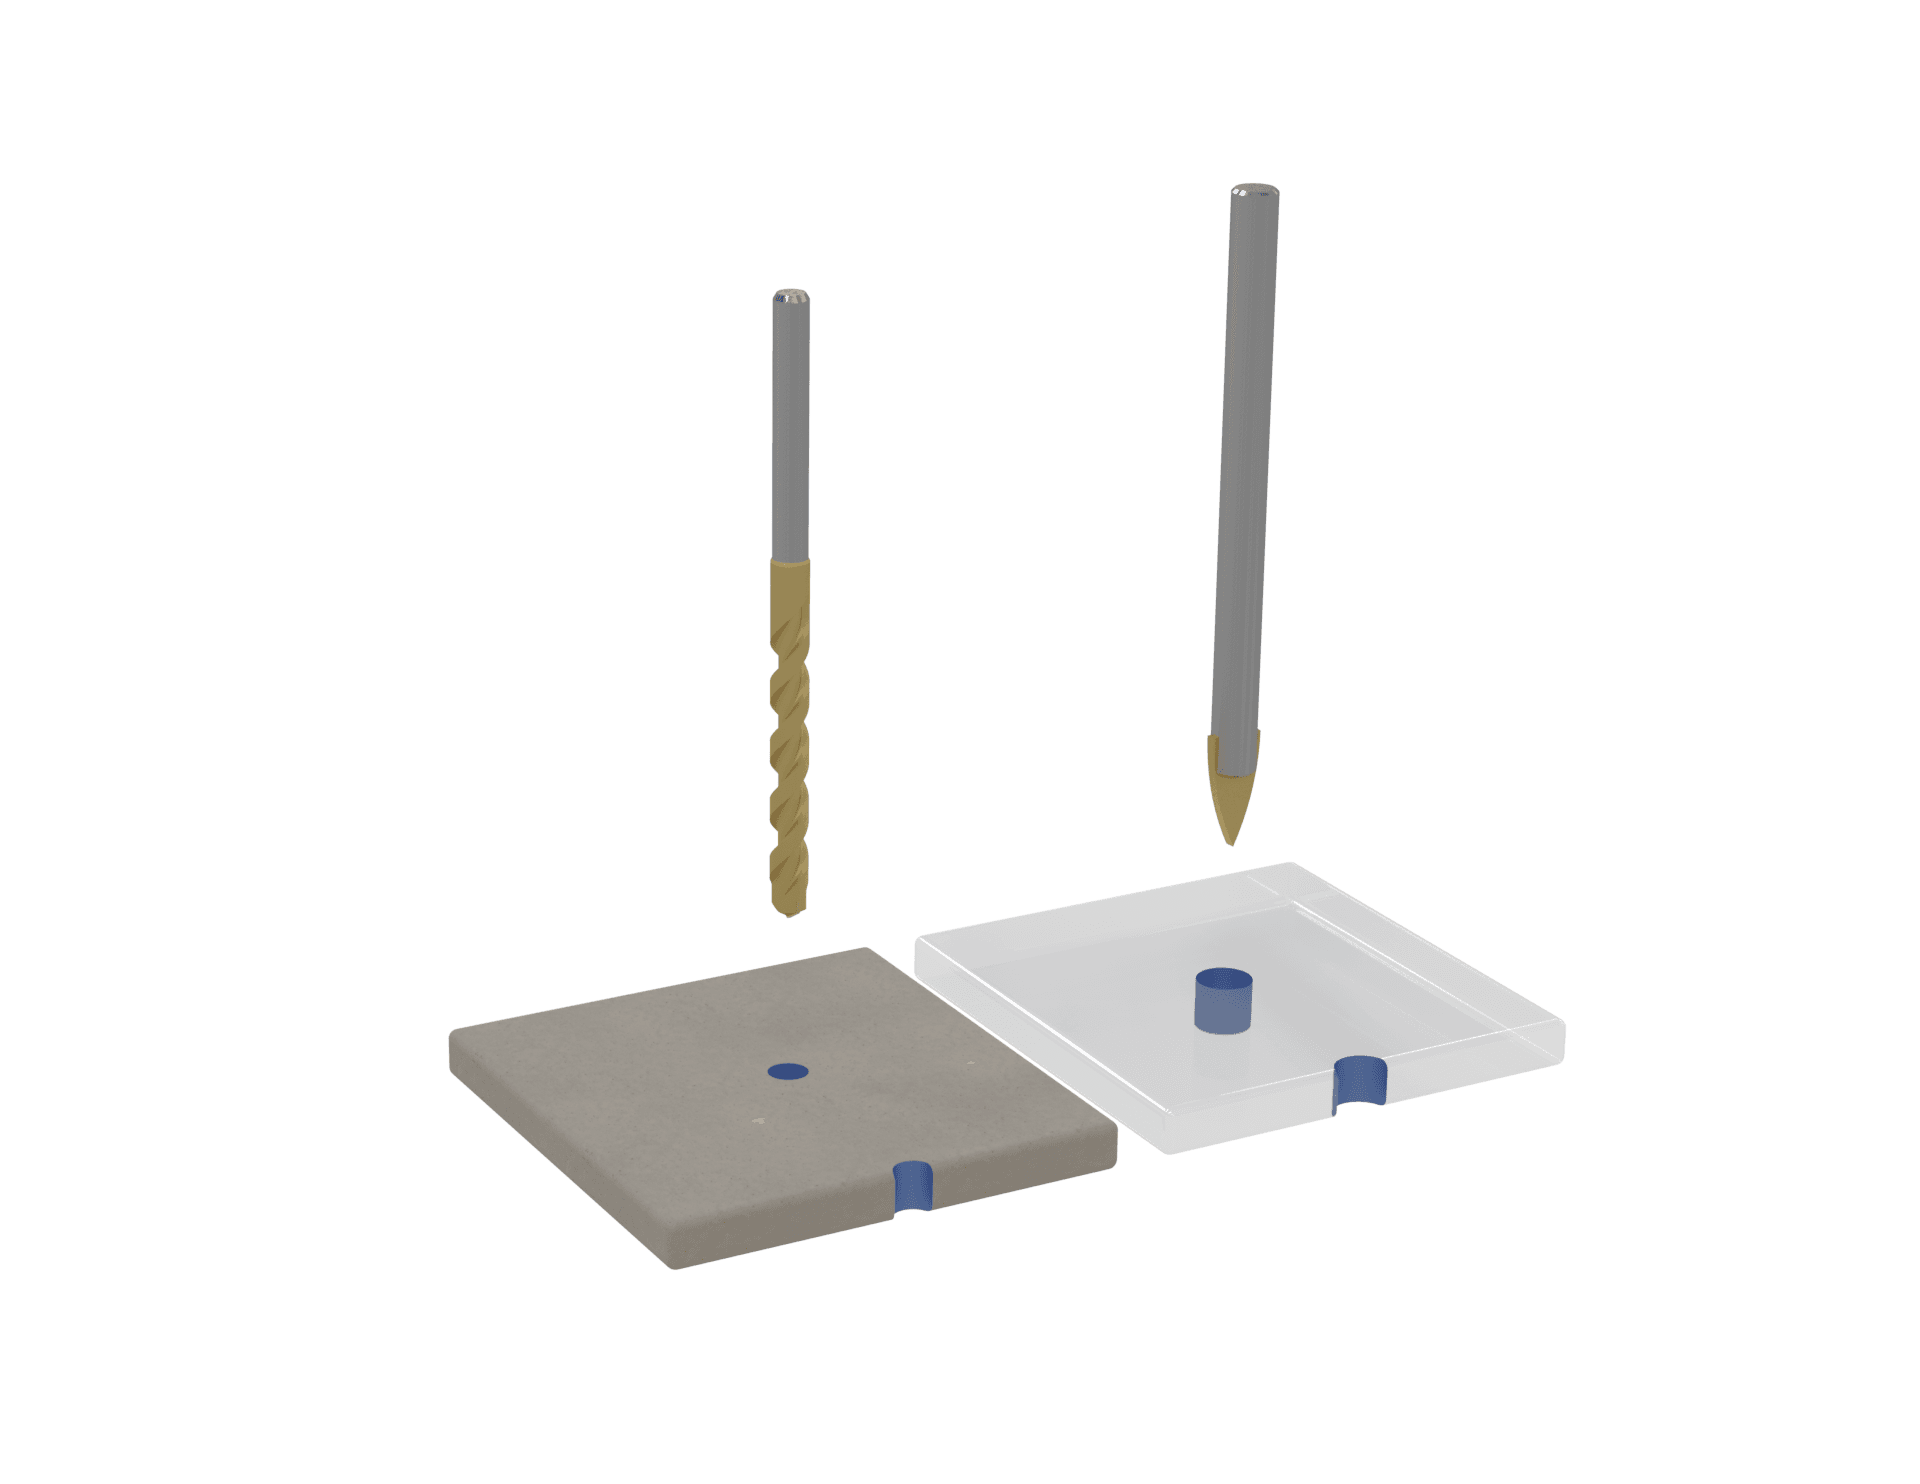
Built to survive abrasive, brittle materials without cracking the workpiece.
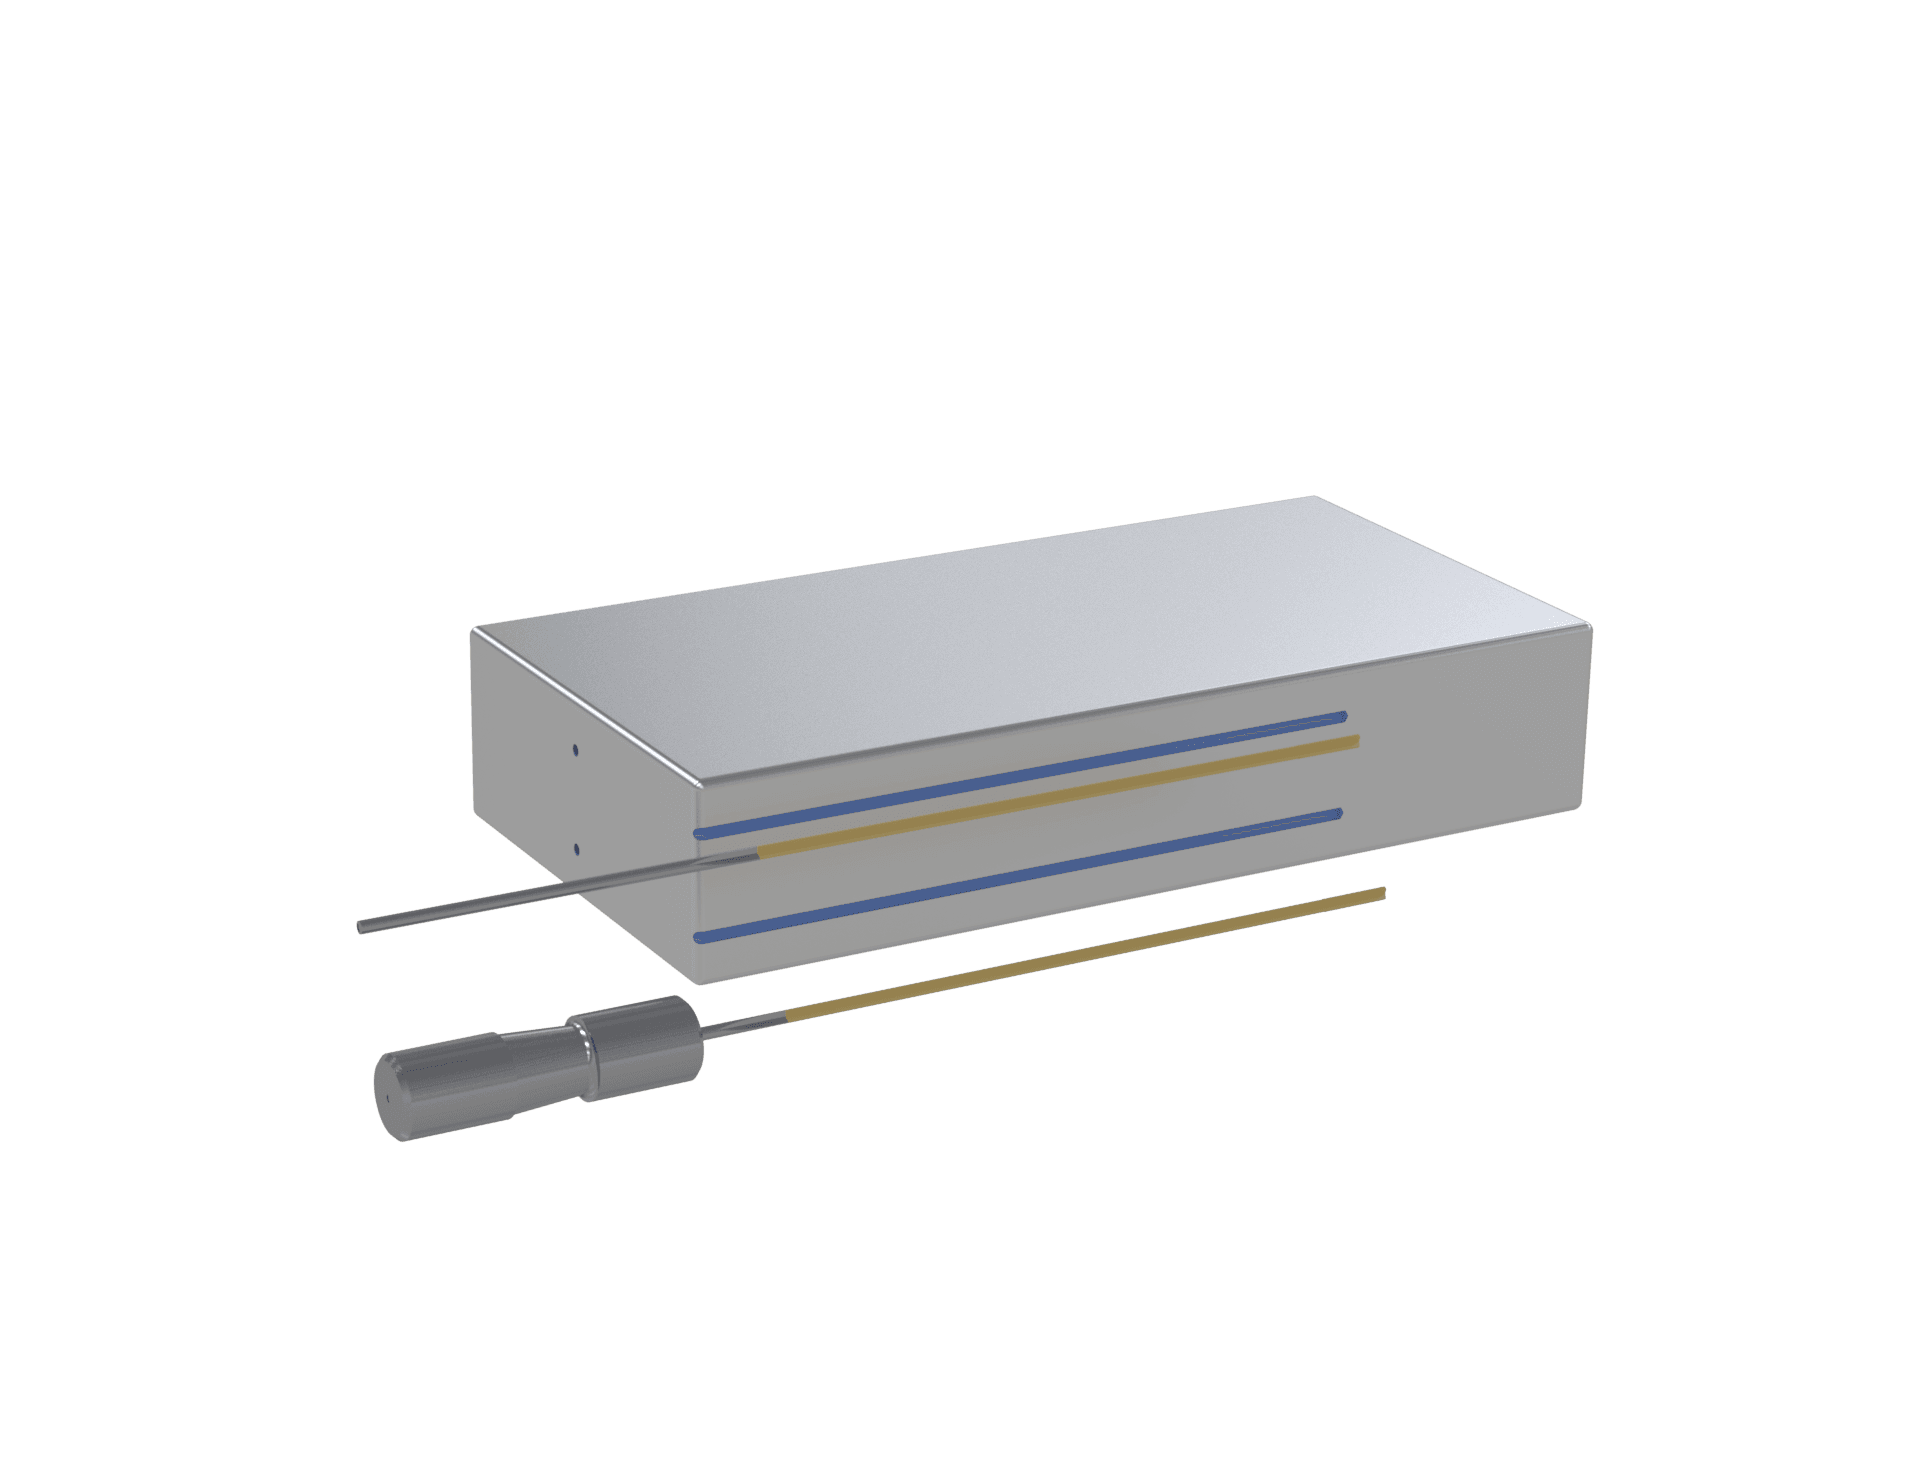
Engineered for extended reach with straight, accurate hole axes.
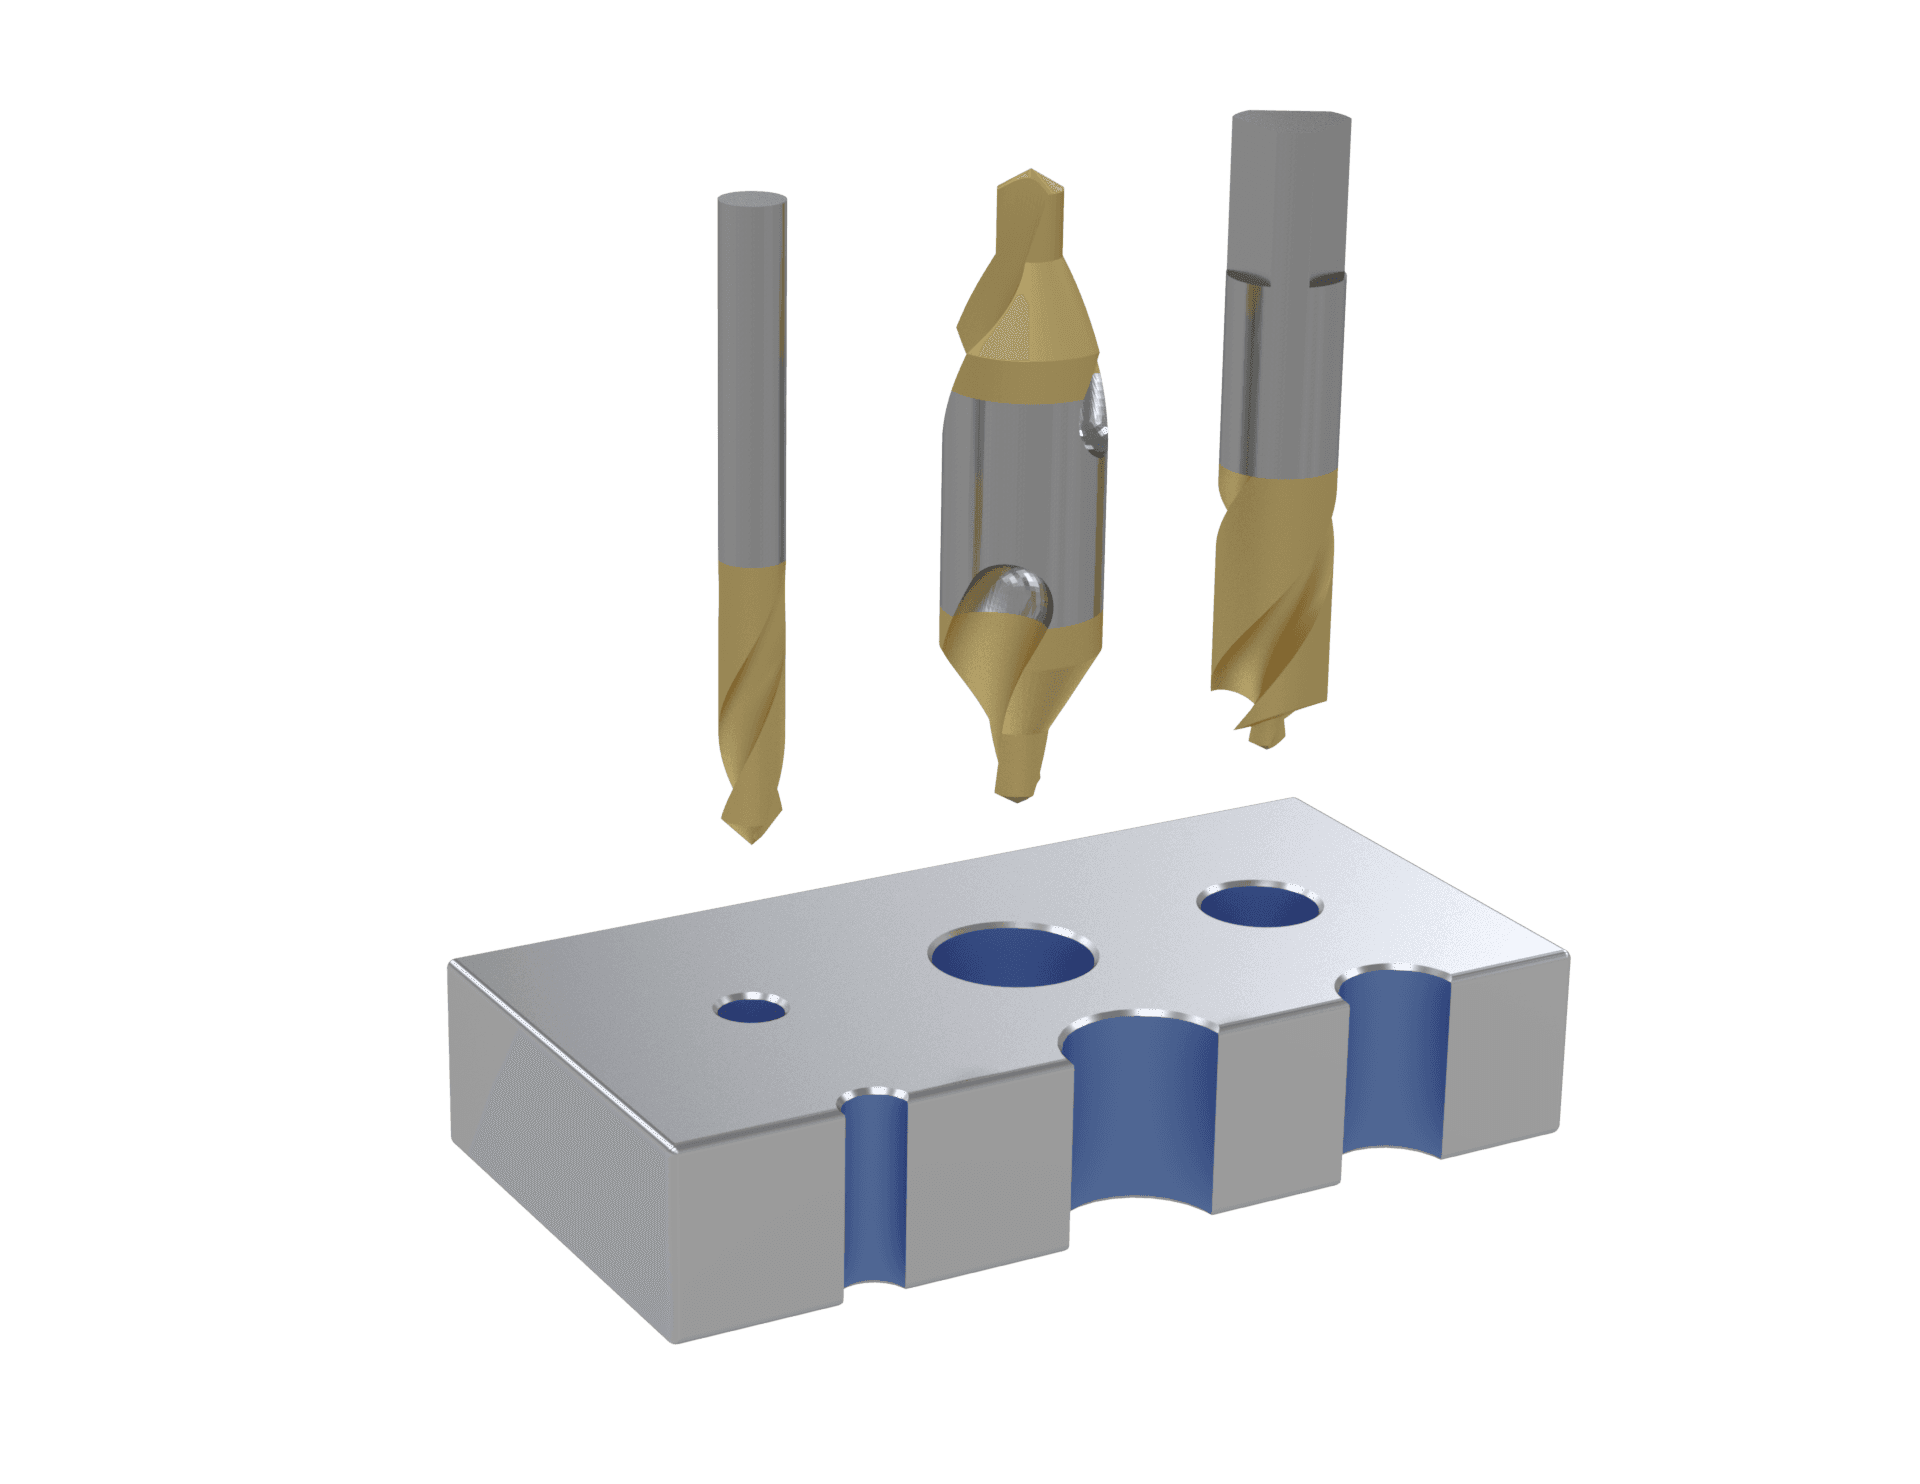
Tools that start and locate holes accurately before finishing operations.
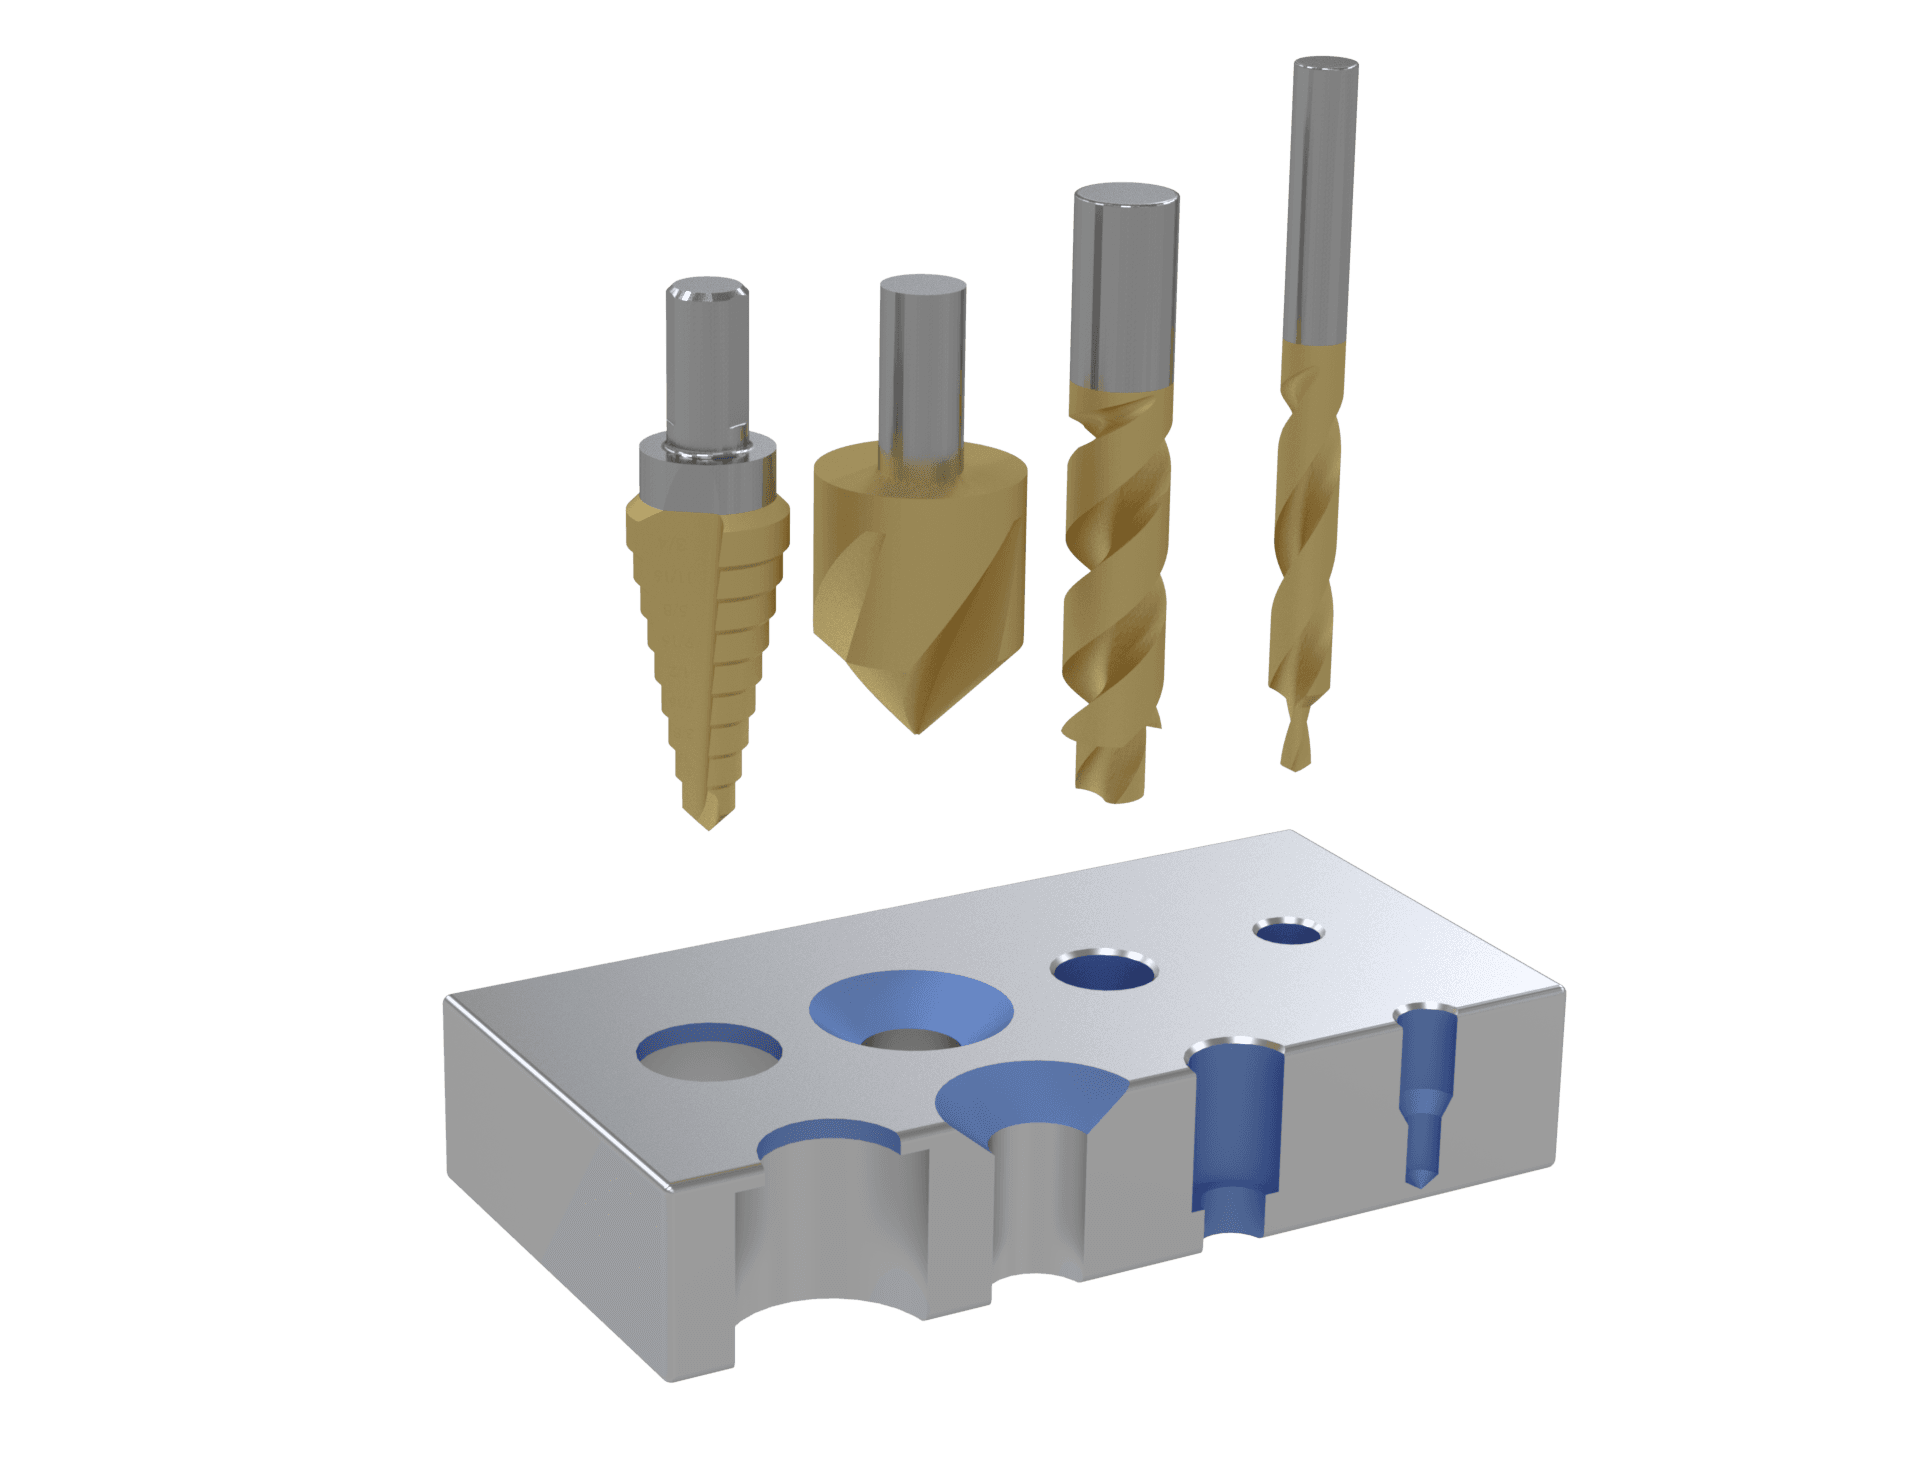
Combined and finishing geometries for shaped or multi-diameter holes.
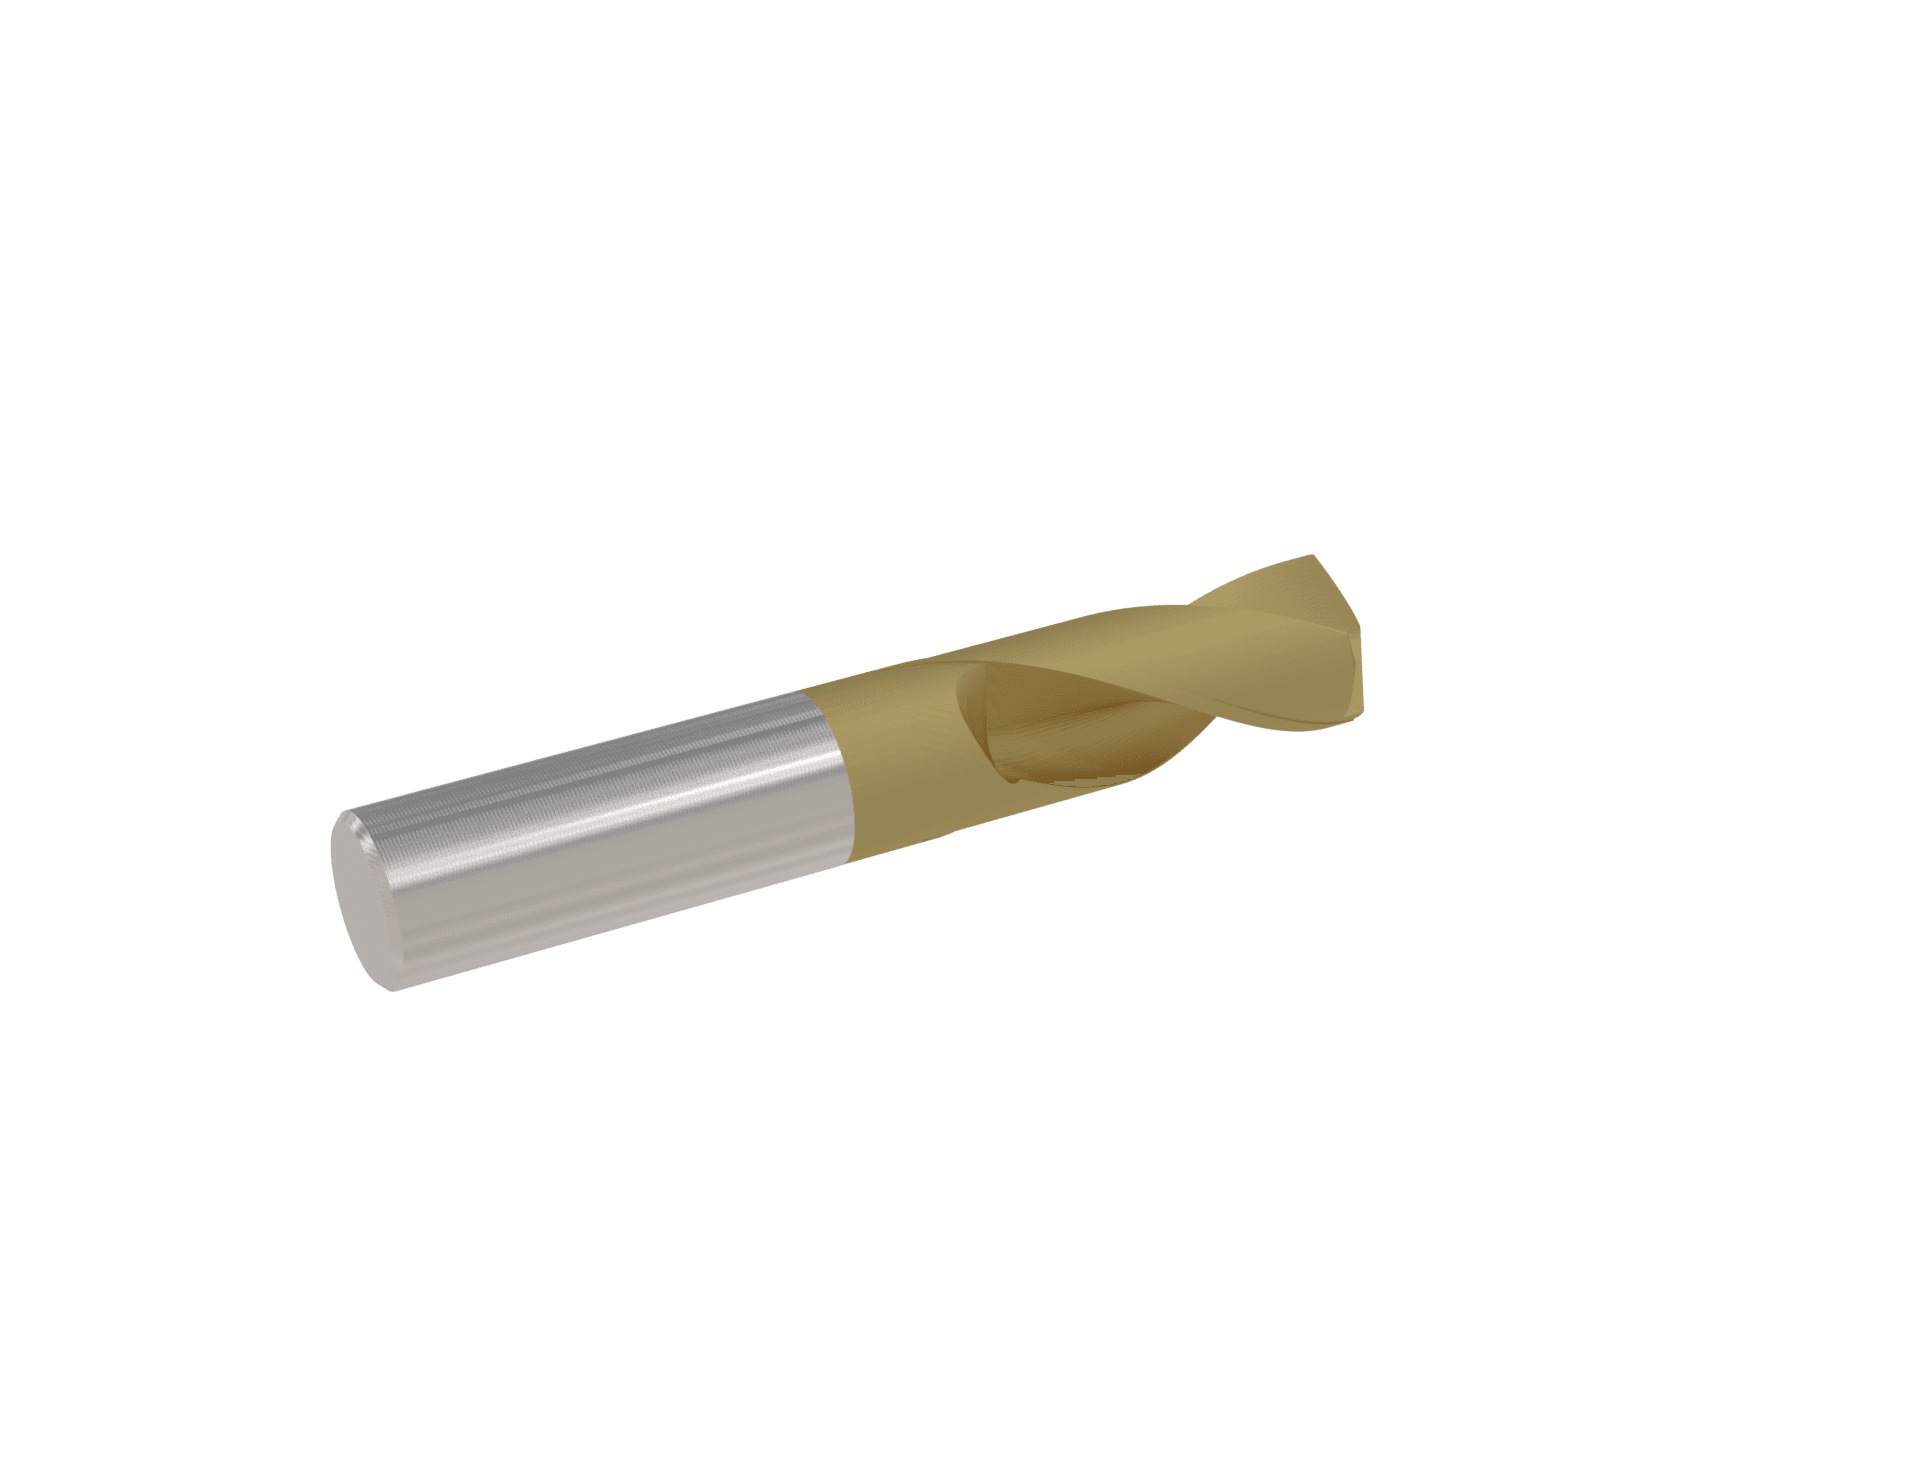
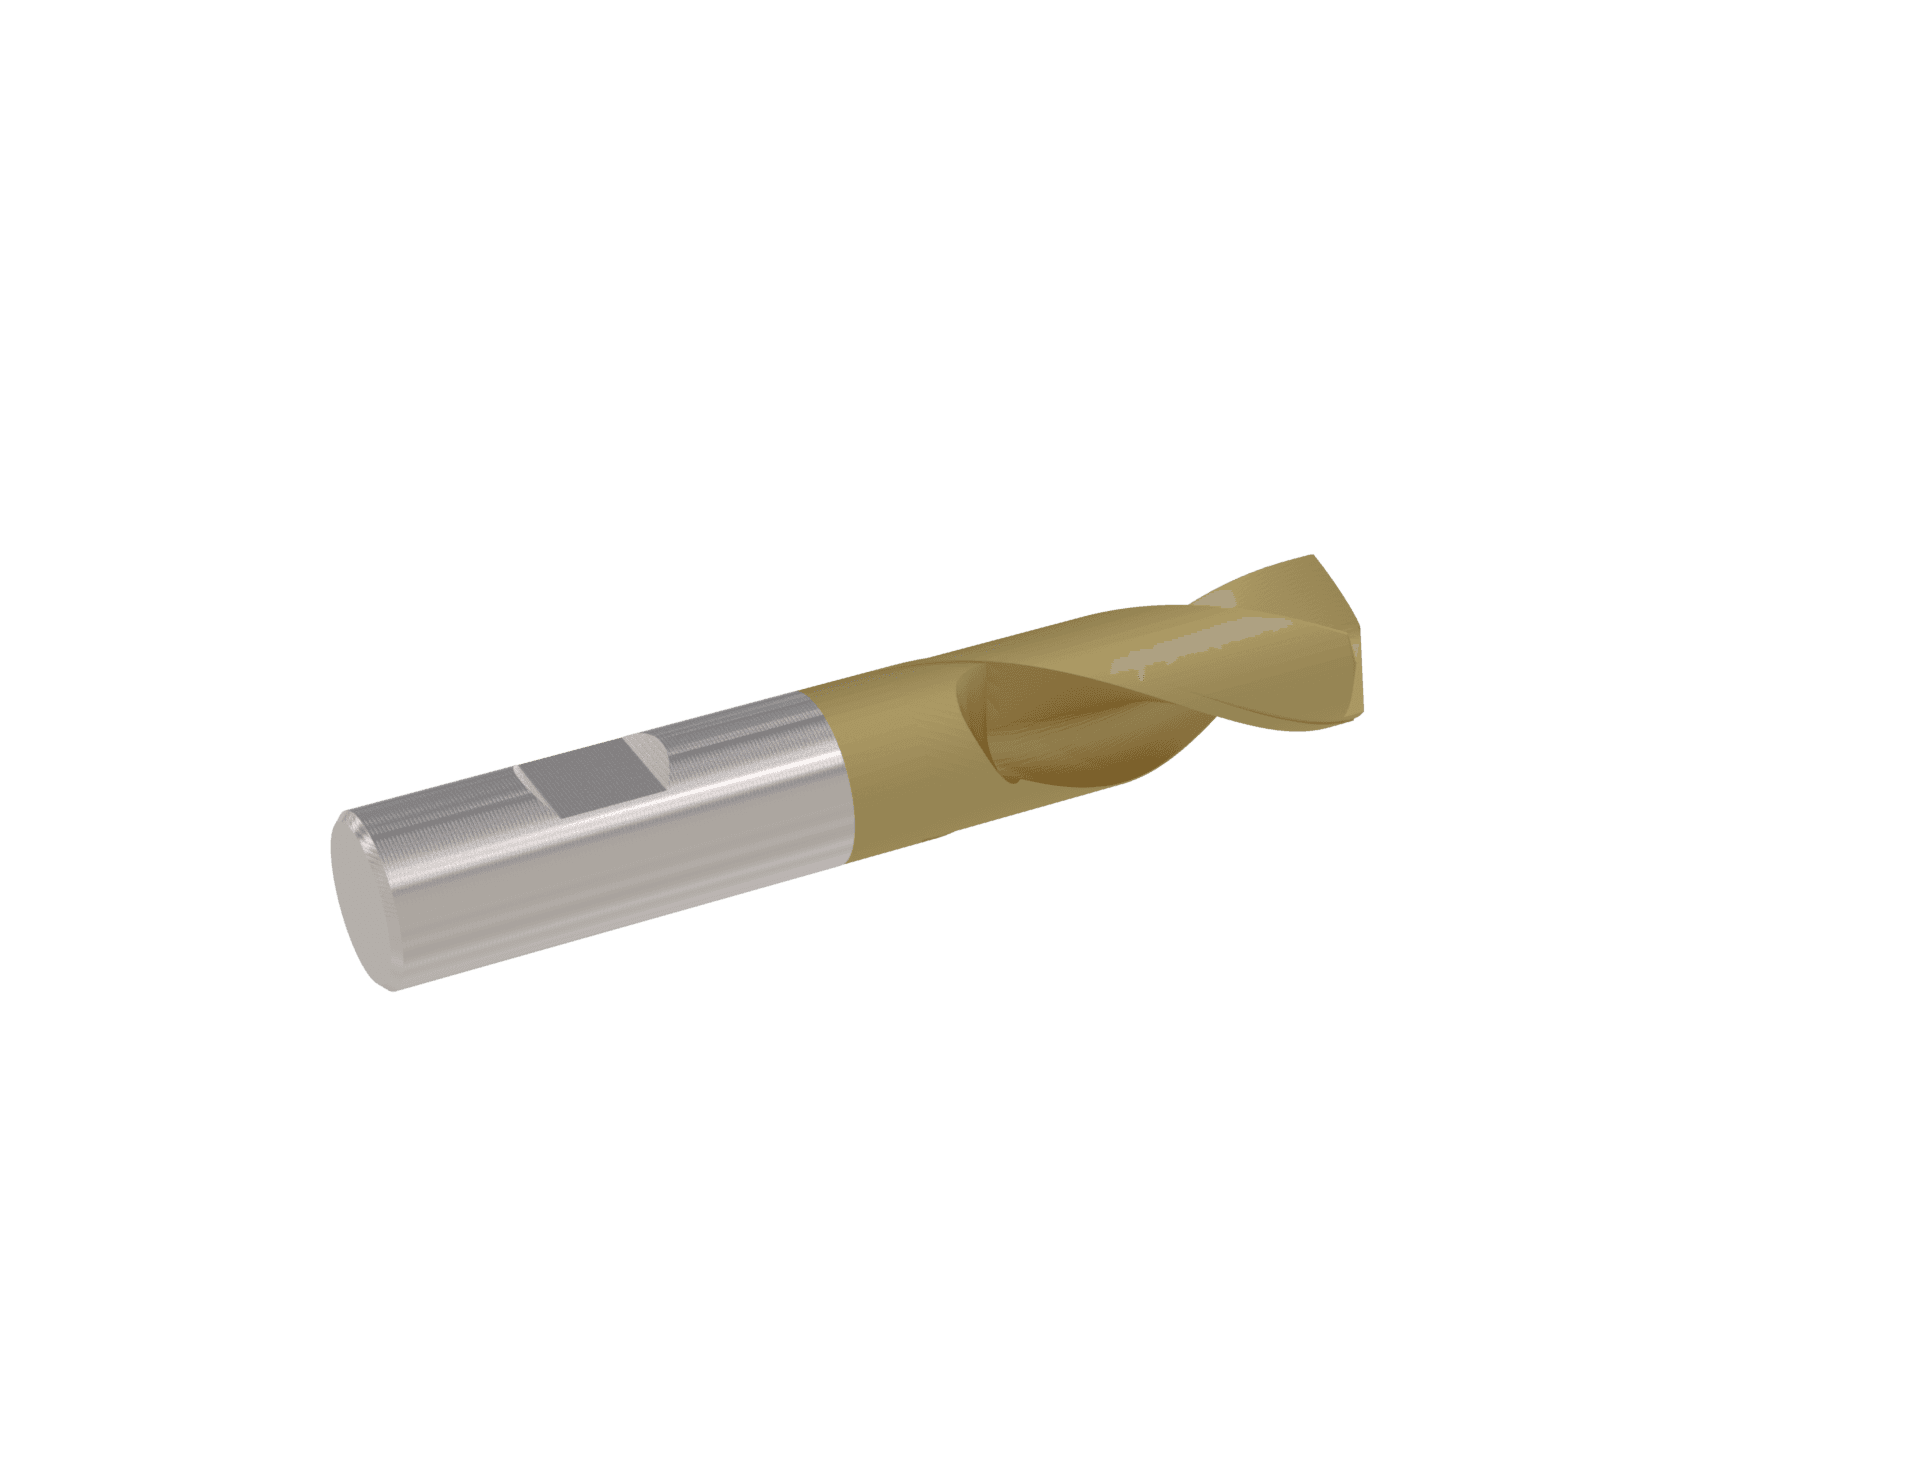
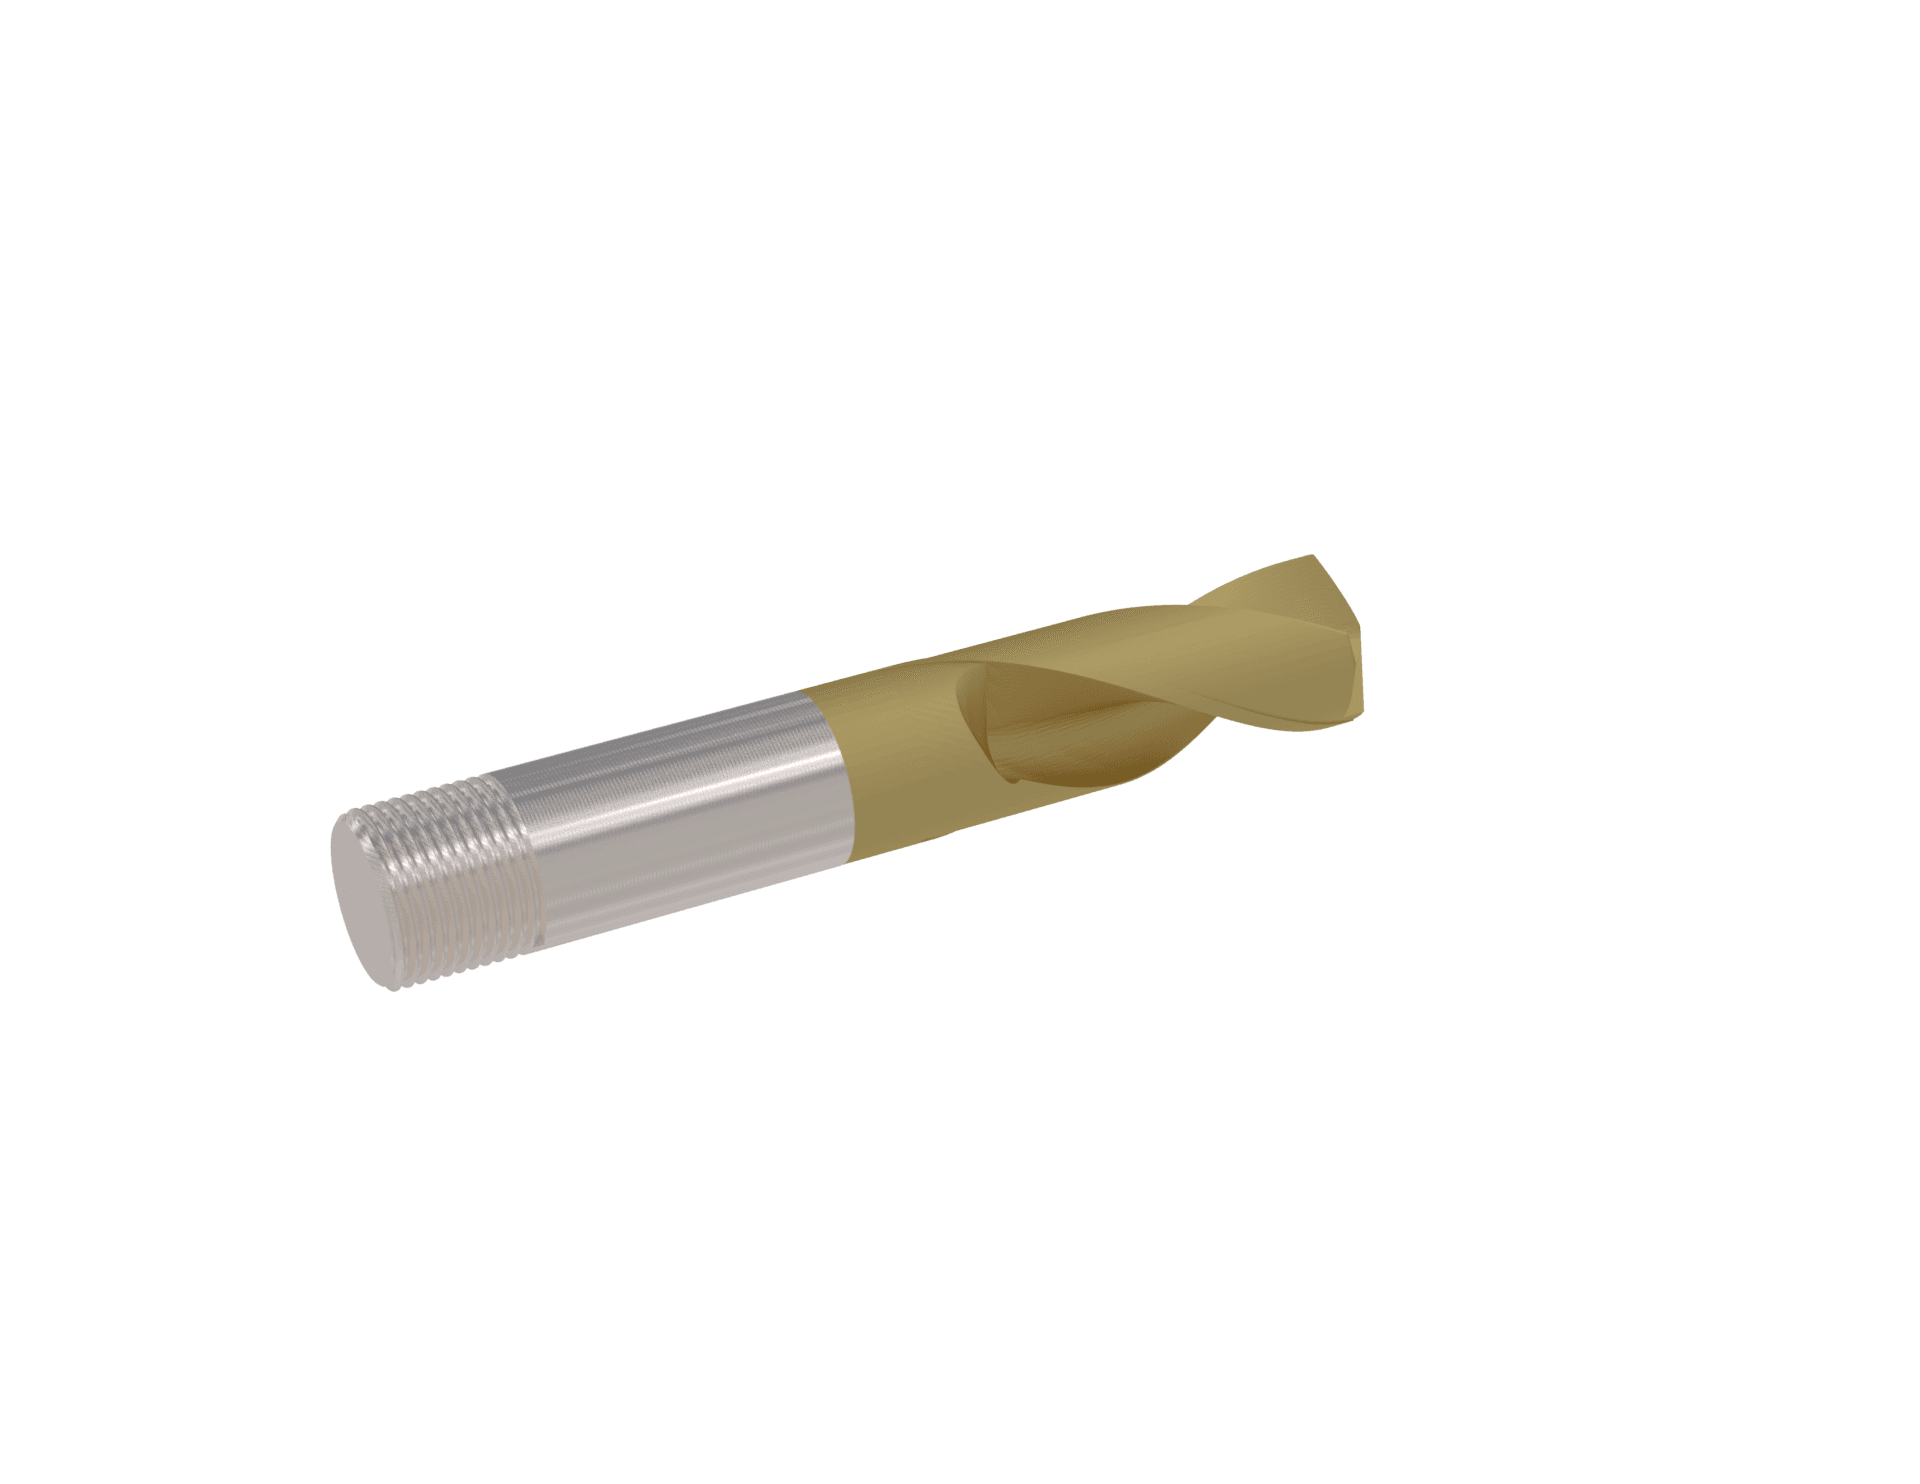
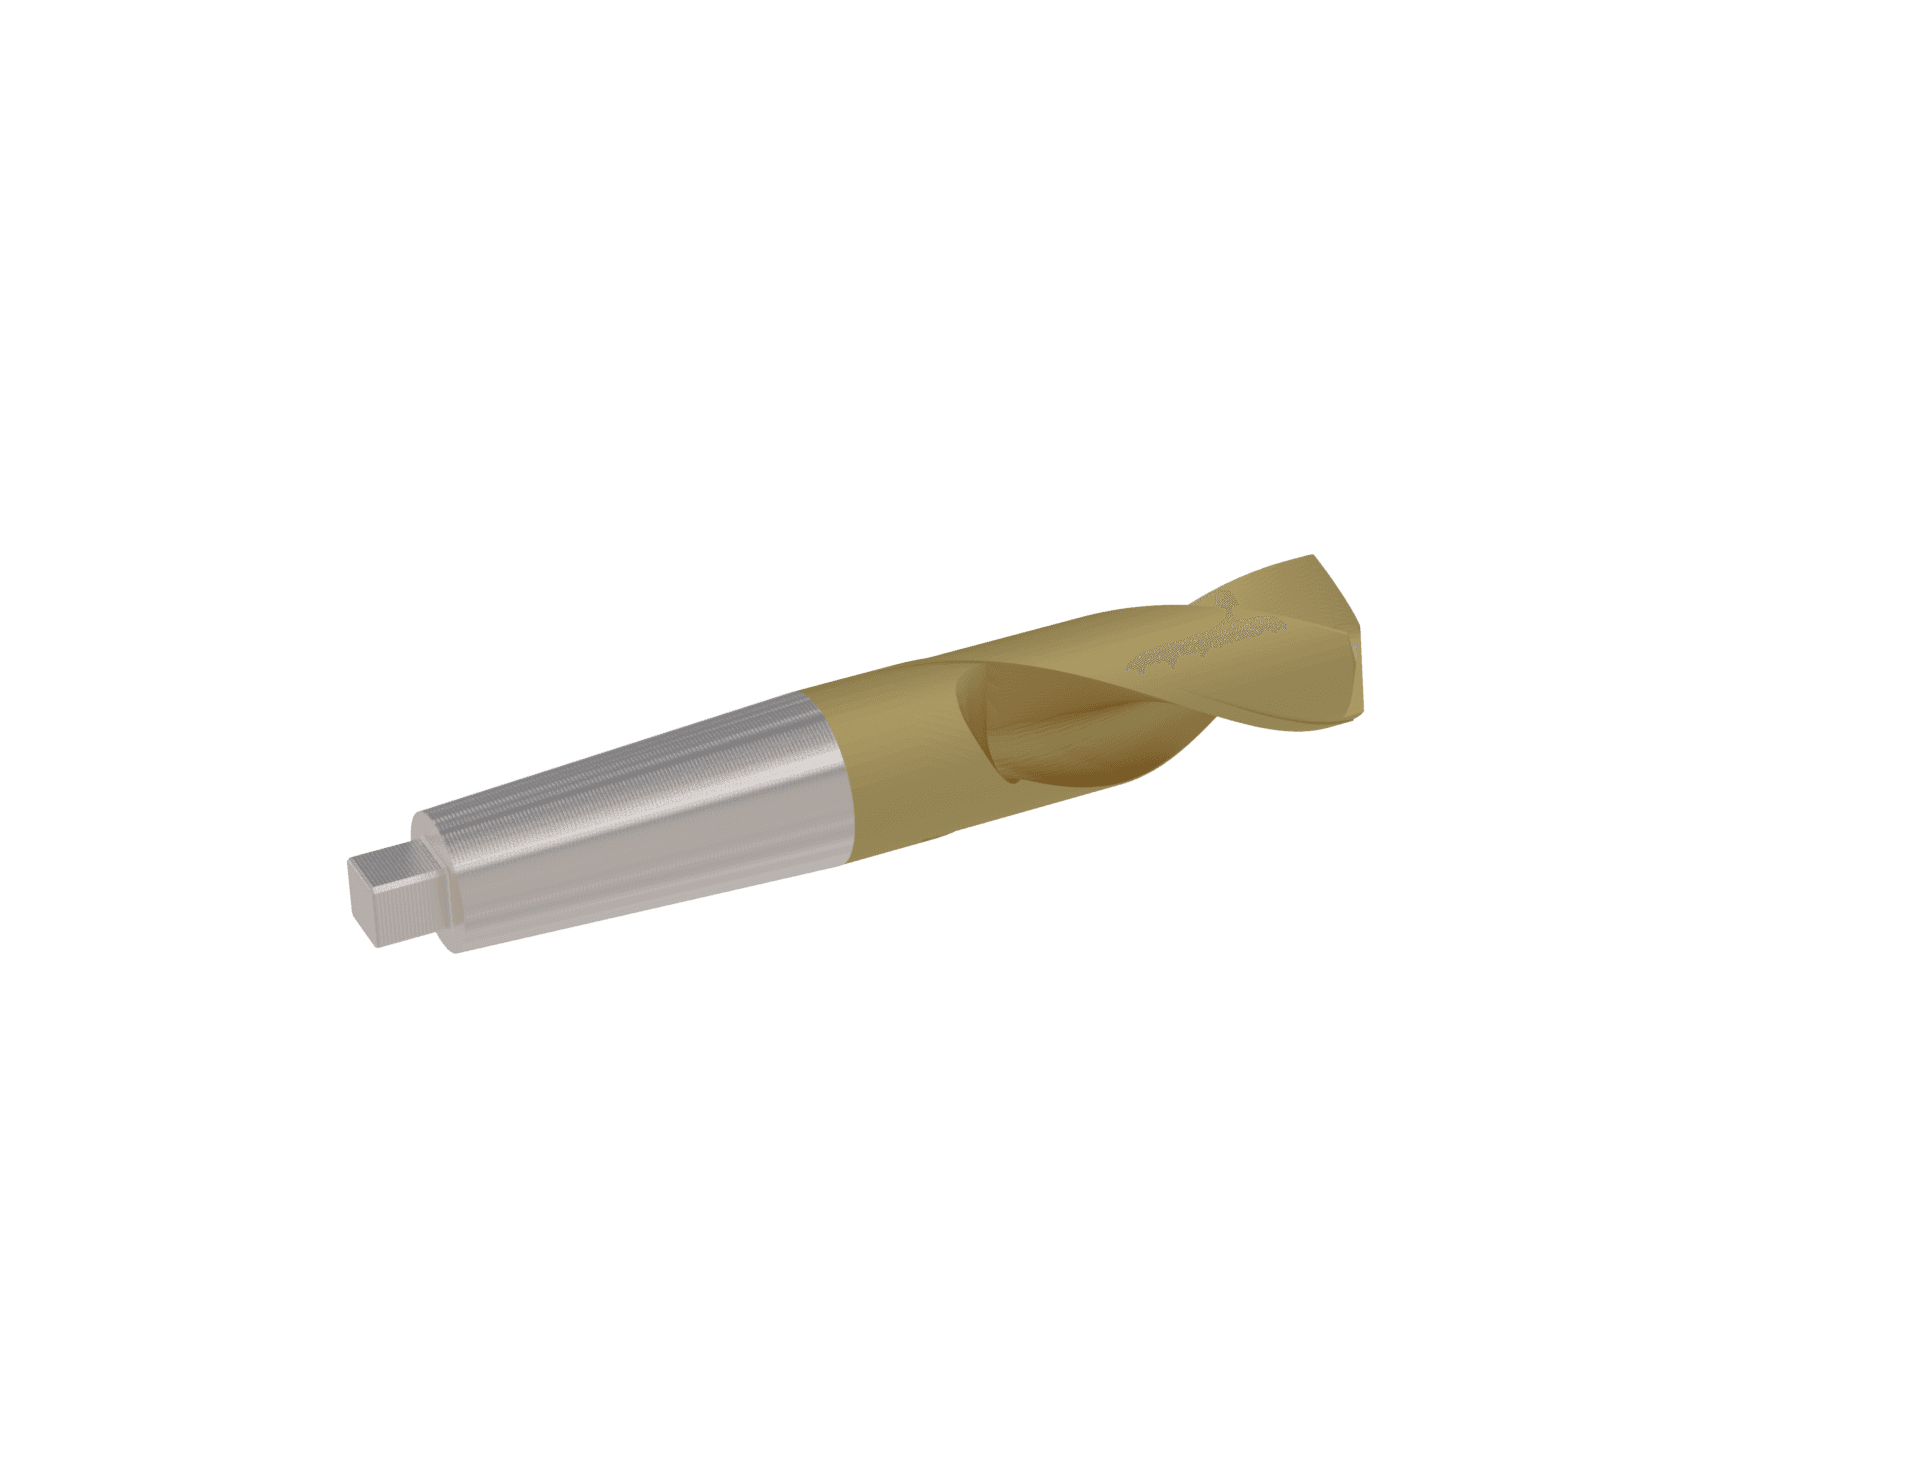
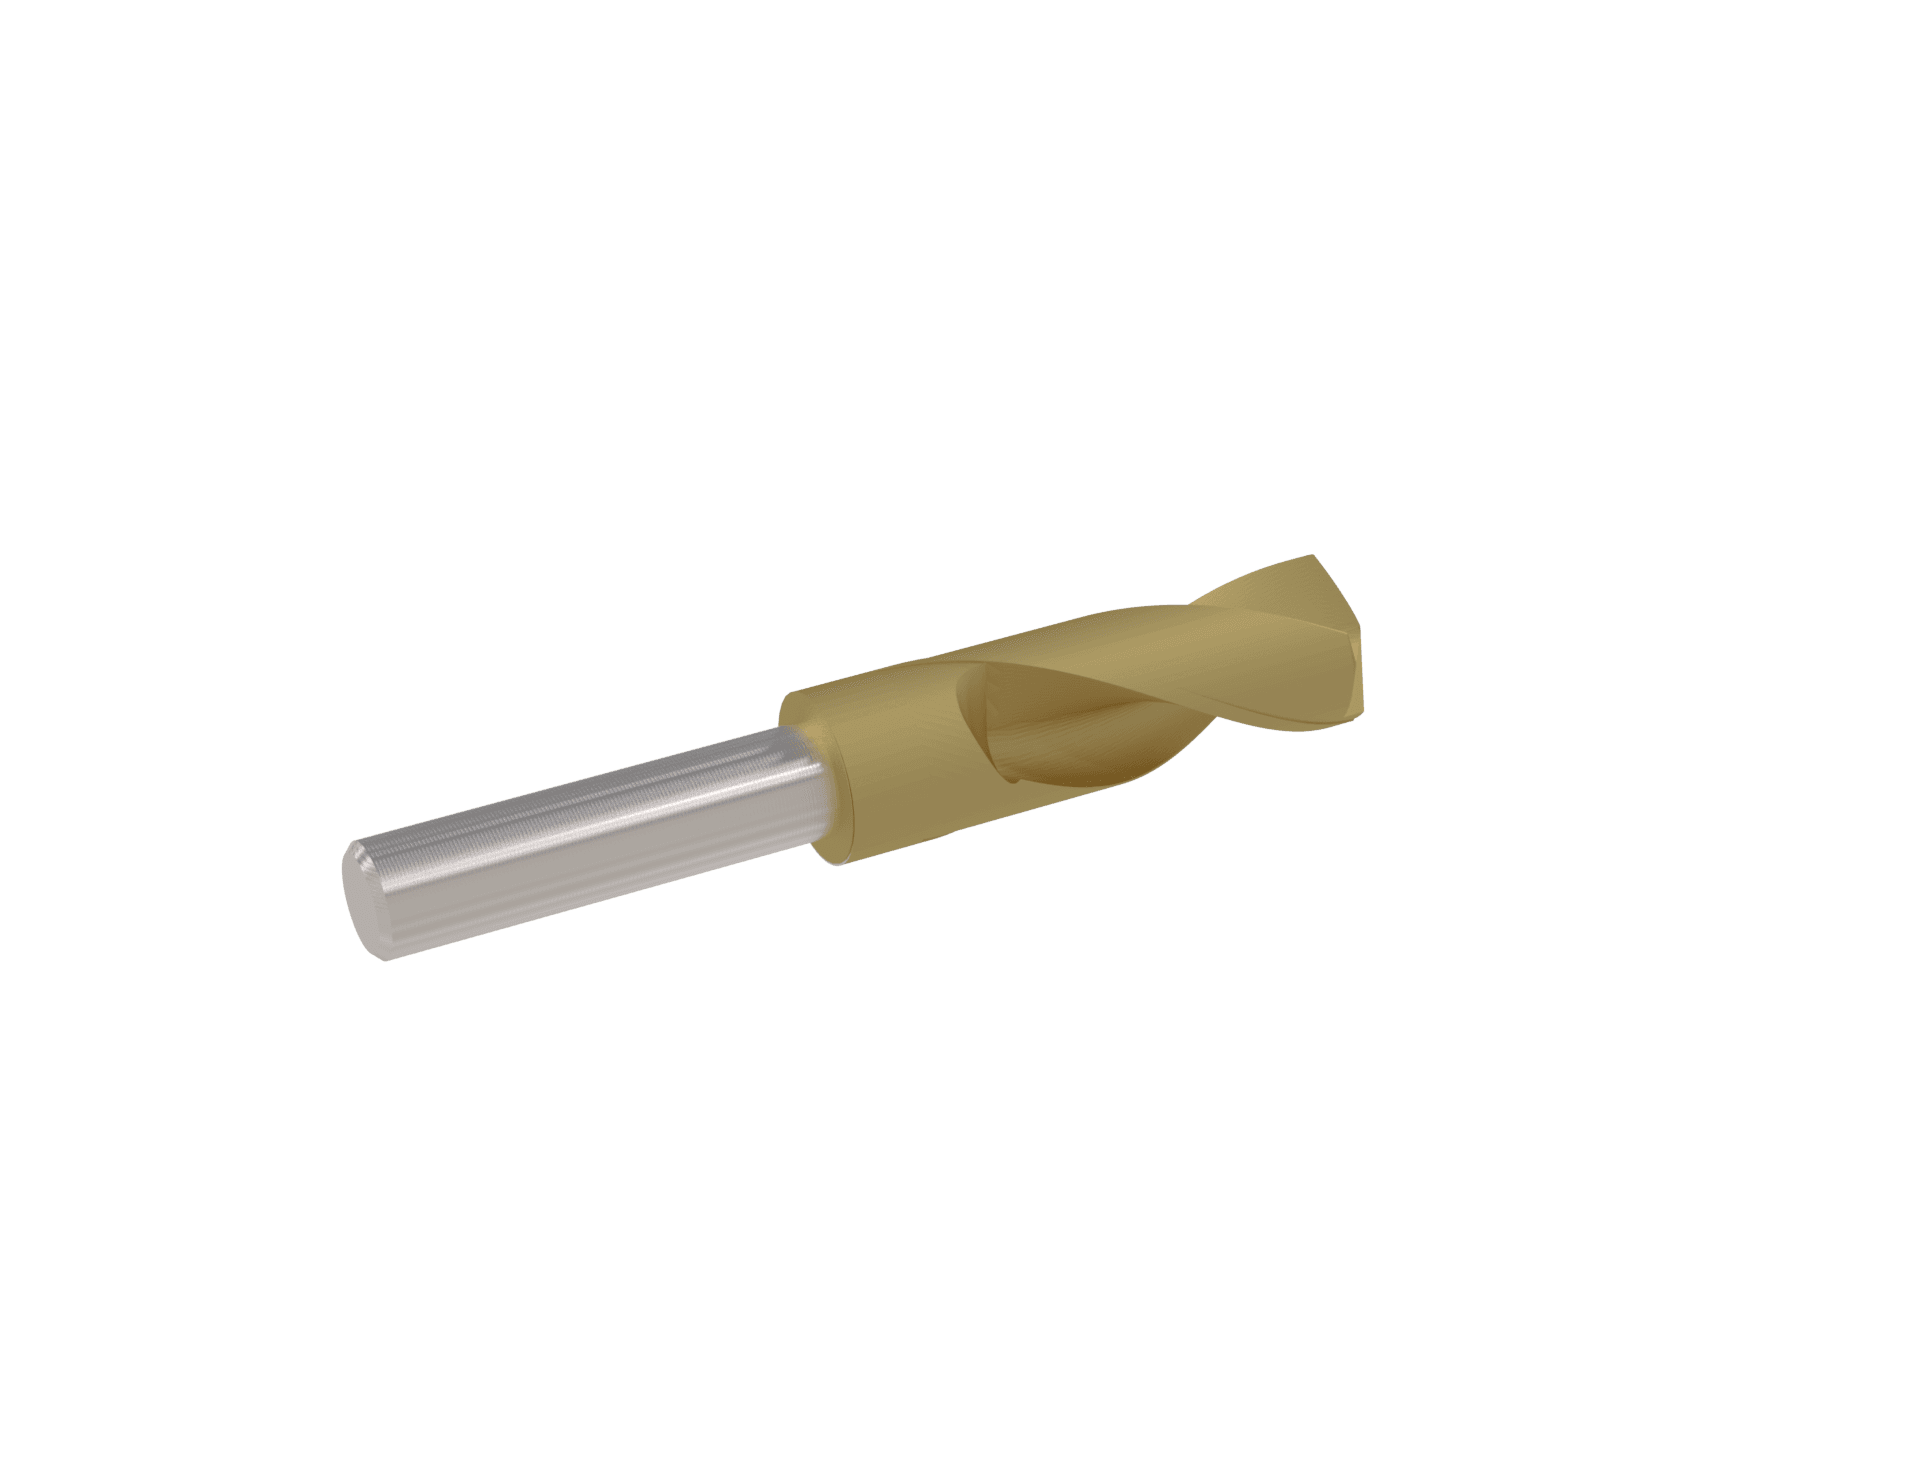
Every Bauron drill can be produced with the shank interface that best matches your machine and holder. Each shank type below is shown with how it mounts and where it performs best.
A flatter point angle, such as 140°, reduces burr formation on exit and creates a shorter chip, making it suitable for tough alloys and automated CNC machining. A sharper point angle penetrates soft materials easily but can cause breakout burrs.
Custom drill bits can combine operations such as step drilling, chamfering, and counterboring in a single step, reducing tool changeover time and cycle cost per part.
Yes. Bauron manufactures bespoke step drills, extended-reach deep-hole drills, specialized coolant-through tools, and custom-diameter drill geometries from technical CAD files.
Through-tool coolant channels deliver high-pressure fluid directly to the chisel point, reducing cutting-zone temperatures and flushing chips up the flutes to prevent chip packing in deep holes.
Looking for custom CNC drill bits, step-drill geometries, or high-feed holemaking solutions for your production line? Consult with a Bauron application engineer.
Bauron works with manufacturers to review tool geometry, substrate, coating, reach, machine conditions, and production requirements for standard and custom CNC tooling.
Submit your requirements